Determining whether a nonconforming sheet metal part should be scrapped or reworked sounds like a simple either-or call. In practice, it is one of the most consequential decisions made on a fabrication shop floor — and one of the least standardized. A bracket that misses its bend angle by half a degree may be perfectly fixable. A part with a cracked weld in a structural joint may not be. The difference between those two outcomes has nothing to do with how severe the defect looks and everything to do with economics, material behavior, and functional risk.
What “Scrap” Means on a Sheet Metal Shop Floor
In manufacturing, scrap refers to a part or material that has been judged permanently unusable. It cannot meet its drawing specifications through rework, and it cannot be shipped even with a documented deviation. The part is removed from the production flow and typically recovered as raw material or discarded.
This definition is narrower than the everyday sense of “waste.” A sheet metal blank left over after nesting is not scrap in the quality sense — it is material remnant. Scrap applies to a part that has already been processed and has failed to meet its requirements.
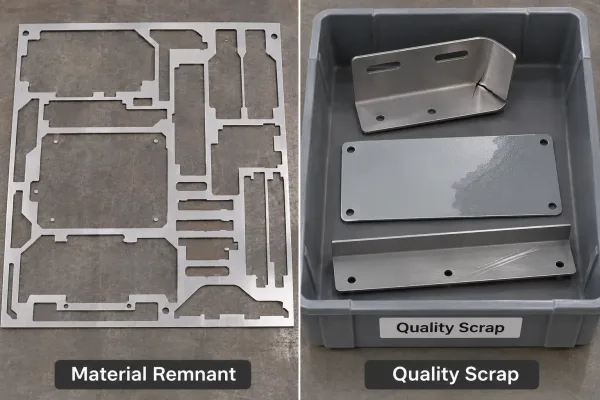
This comparison distinguishes material remnant (the leftover sheet skeleton after nesting) from quality scrap (processed parts that failed inspection and cannot be reworked).
Scrap, Rework, or Repair: Three Different Outcomes
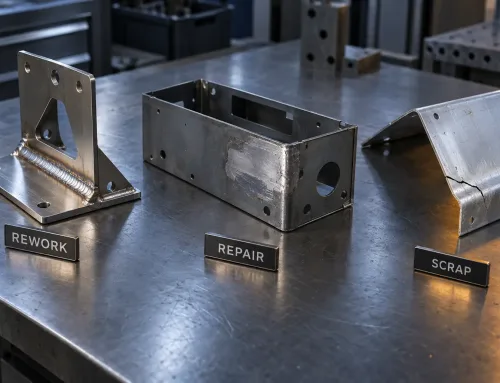
When inspection identifies a nonconforming part, three dispositions are possible. Each path has a different endpoint.
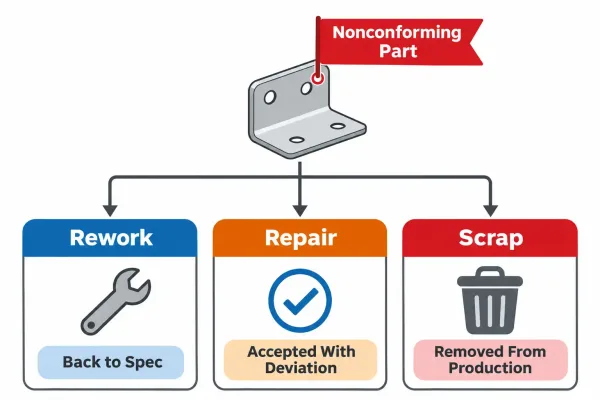
This diagram illustrates the three possible dispositions for a nonconforming part — rework back to spec, repair with a documented deviation, or scrap — and their distinct endpoints.
| Disposition | What Happens | Endpoint | Typical Trigger |
|---|---|---|---|
| Rework | Additional operations bring the part back to full drawing specification | Part meets all original requirements | Deviation correctable by a secondary operation |
| Repair | Part is restored to functional condition, often with a buyer concession | Part is usable but carries a documented deviation | Cosmetic defect or minor out-of-tolerance on a non-critical dimension |
| Scrap | Part is removed from production permanently | Part is destroyed or sold as raw material | Defect cannot be corrected economically or safely |
Rework returns the part to its original specification. If a powder-coated panel has a thin spot, stripping and recoating is rework — the finished part should meet the same film-thickness callout as a first-run part.
Repair restores function but accepts a deviation. If a flange is slightly out of flat but the assembly still seals correctly, the buyer may accept it with a written concession. The part ships, but it does not fully meet the drawing.
Scrap means the part is done. No further investment will bring it into specification, and shipping it as-is is not acceptable.
When to Scrap Rather Than Rework: A Decision Framework
The choice between rework and scrap is rarely about the size of the defect. It is about whether further processing makes economic and engineering sense. Three tests structure the decision.
The Economic Test — When Rework Costs More Than Remaking
Every rework operation carries a cost: labor, machine time, consumables, and re-inspection. When the cumulative cost of rework approaches or exceeds the cost of producing a replacement part, scrap is the rational choice.
For simple laser-cut parts, this threshold is often reached quickly. If a part has already been bent and welded, the cost of cutting, forming, and joining a replacement may be comparable to the labor cost of grinding out a weld and re-welding. For complex subassemblies with multiple fabricated components, the math shifts in favor of rework because a replacement carries more downstream cost.
A practical rule: if rework requires more than one corrective operation, or if it involves undoing a permanent process such as welding, swaging, or adhesive bonding, compare the estimated rework hours against the cycle time for a replacement part before committing.
The Structural and Safety Test — When Rework Compromises Integrity
Some defects cannot be corrected without affecting structural performance. Cracks in load-bearing welds, excessive thinning from repeated bending, and deformation beyond the material’s elastic limit are common examples in sheet metal work.
When a part has been bent past its minimum inside radius and cracked, bending it back does not restore the original grain structure. The work-hardened zone remains, and the part is now more likely to fail in service. Rework in this case is not just uneconomical — it is unsafe.
Any part destined for a structural, pressure-containing, or safety-critical application should be scrapped if rework would leave residual stress, micro-cracking, or wall thinning below the design minimum.
The Surface and Functional Test — When Rework Cannot Restore Performance
Not every defect is structural, but some affect function in ways that rework cannot fix. A machined mounting surface scratched beyond the specified Ra value cannot be restored by polishing if base material has been removed. A plating layer with adhesion failure cannot be corrected by re-plating over a contaminated substrate.
If the defect lies on a surface that performs a sealing, electrical, or wear function, and the rework process cannot guarantee the original callout, the part should be scrapped.
What Causes Scrap in Sheet Metal Fabrication
Scrap in sheet metal production has identifiable causes at each process stage:
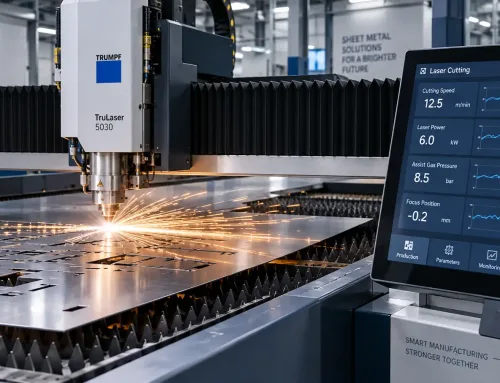
- Cutting and blanking — incorrect nesting, wrong material thickness loaded, laser power drift causing incomplete cuts or excessive dross
- Forming and bending — over-bending beyond springback compensation, cracks at tight radii, tooling marks on cosmetic surfaces
- Welding and joining — burn-through on thin gauge, porosity in structural welds, misalignment that cannot be corrected after the joint is made
- Surface treatment — coating adhesion failure, film thickness out of specification on critical areas, contamination before finishing
- Incoming material — out-of-tolerance sheet thickness, mill surface defects, mixed material grades
Many scrap events trace back to a single upstream decision: a missing tolerance on the drawing, an unverified material substitution, or a setup that was never validated with a first article.
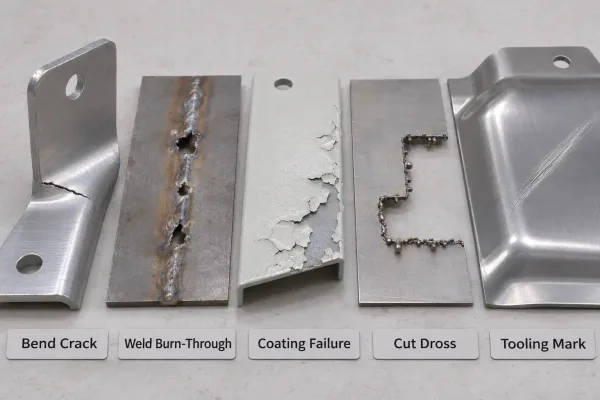
Five representative sheet metal defects that commonly lead to scrap: bend cracking, weld burn-through, coating adhesion failure, incomplete laser cutting with dross, and tooling marks on cosmetic surfaces.
How Scrap Decisions Affect Cost and Yield Rate
Direct and Hidden Cost of a Scrapped Part
The cost of a scrapped part is not limited to raw material. By the time a part reaches final inspection and fails, the shop has already invested in cutting, forming, joining, finishing, and inspection labor. Material cost is typically a minority of the total value added.
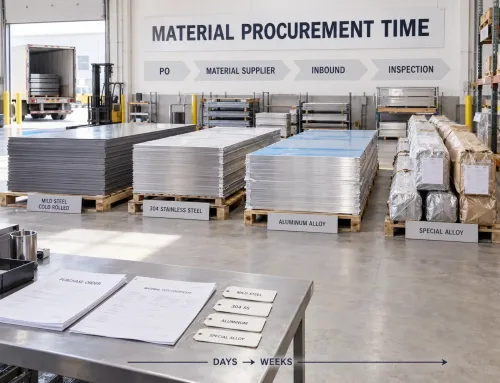
Hidden costs amplify the loss: production schedule disruption, replacement material procurement time, and re-inspection of the replacement batch. If scrap occurs late in the process, the effective cost can reach three to five times the material value.
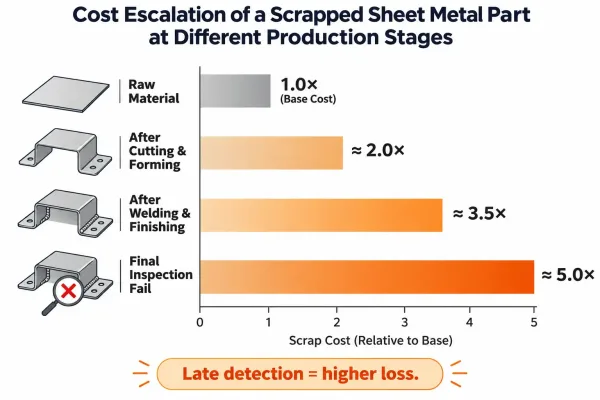
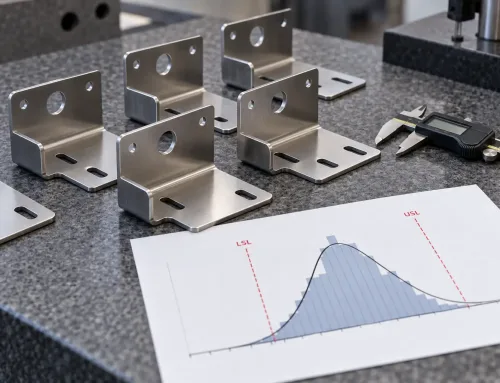
This chart illustrates how the cost of a scrapped part increases as it moves through production — late-stage scrap at final inspection can cost up to five times the raw material value.
How Scrap Feeds Into Yield Rate
Yield rate measures the percentage of started parts that reach finished-good status. Scrap directly reduces the numerator. A run of 100 parts with 5 scrapped yields 95 — a 95% yield rate.
The impact compounds when scrap is discovered late. If 5 defective parts are caught at the forming stage, the remaining 95 still move through welding and finishing on schedule. If the same defects surface only after coating, the entire batch may require re-inspection and the delivery date is at risk.
The earlier a defect is caught, the more options remain — rework, repair, or targeted replacement. Late-stage scrap eliminates those options and maximizes the loss.
How Buyers Can Reduce Scrap Risk Before Production Starts
Much of the scrap in sheet metal fabrication is preventable at the specification stage. Buyers and design engineers can reduce risk before the RFQ is even sent:
- Mark critical-to-quality (CTQ) dimensions explicitly — distinguish functional requirements from general tolerances so the fabricator knows where rework is acceptable and where it is not
- Define rework boundaries in the PO or drawing notes — state which deviations can be accepted with a concession and which require a scrapped part
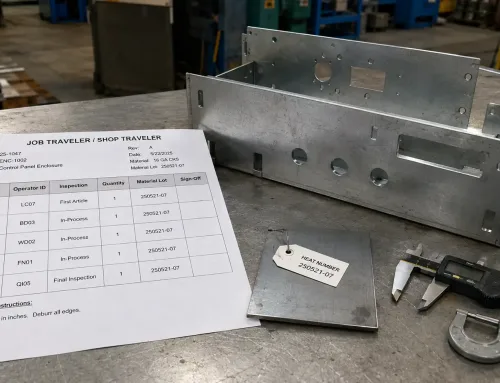
- Require first article inspection (FAI) — a validated first piece prevents batch-level scrap from systematic errors
- Specify material substitution rules — clarify whether an equivalent grade is acceptable, or the entire batch is at risk when the specified material is unavailable
These steps cost nothing at the quoting stage and can prevent significant scrap exposure during production.
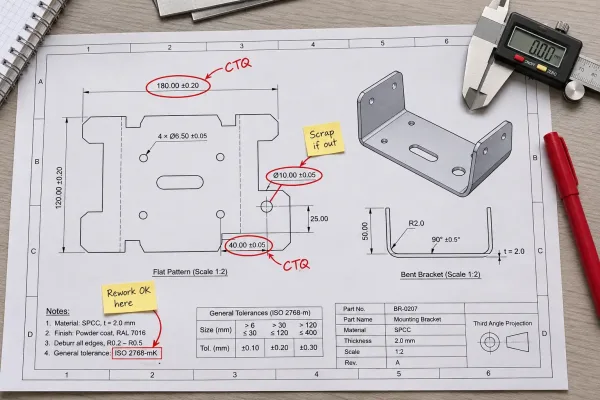
A drawing example showing how to mark critical-to-quality (CTQ) dimensions and define rework boundaries directly on the print — a preventive measure that reduces scrap risk before production starts.
FAQs
For best results, define your scrap and rework criteria at the drawing and RFQ stage — not after the first batch arrives. A short conversation with your fabricator about which deviations are acceptable and which are not can prevent the majority of scrap-related cost and schedule surprises.