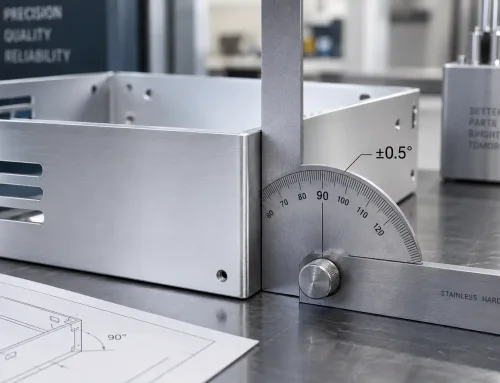
You have a drawing package ready and three quotes on your screen. The prices sit within 15% of each other. Every supplier says they can hold your tolerances, every website shows clean cut parts, and every contact replies within a day. On paper, the shortlist looks finished. It is not.
What separates a laser cutting provider that repeats your part for two years from one that delivers a good first batch and then drifts is rarely visible in the quote documents. It is visible in the evidence each supplier is willing to produce. Evaluating a sheet metal laser cutting service provider is not a certificate check — it is a staged process of collecting proof that the shop can cut your specific part, in your material and thickness, to the dimensions and edge condition your product needs. This guide follows that evidence chain from RFQ response to production release.
Evaluation Starts With Your Part, Not Their Machine List
Most supplier evaluation templates were written for general fabrication: certificates, machine inventory, years in business, facility size. Those data points matter, but they answer the wrong question here. A shop can own five fiber lasers and still mishandle a 1 mm aluminum flange, because the risk in laser cutting is not machine ownership — it is how process limits interact with your part geometry.
Start by writing down what “qualified” means for your job: material grade and condition, thickness range, general and critical tolerances, edge condition (as-cut, deburred, or dressed), cosmetic areas, and secondary operations such as bending, tapping, hardware insertion, welding, or coating. Each item filters suppliers differently. A provider comfortable with 12 mm mild steel plate may run thin stainless poorly; a shop built for high-volume flat parts may price low-volume weldments punitively.
That definition is the measuring stick for every later step. You are not evaluating whether a supplier is good in general. You are evaluating whether they can prove — on paper and on parts — that they can repeat your specific requirements.
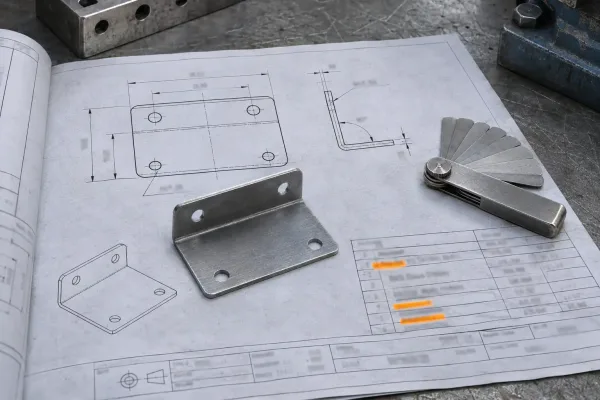
Evaluation starts with the part: the drawing defines material, thickness, tolerance class, edge condition, and secondary operations.
What a Quote and DFM Feedback Should Reveal
Before any metal is cut, two documents already expose a supplier’s engineering depth: the quotation and the DFM (design for manufacturability) feedback attached to it. Read both as capability evidence, not as paperwork.
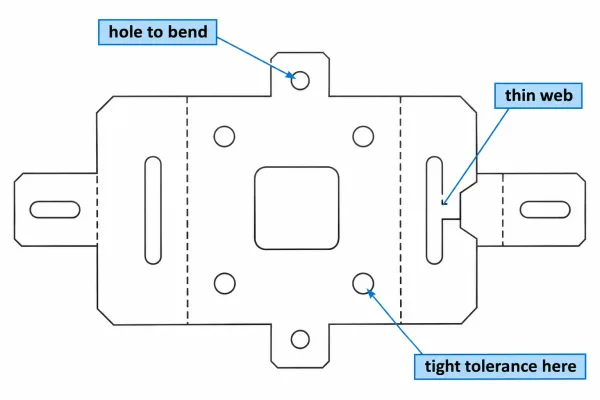
Feature-level DFM feedback names specific drawing features instead of giving generic approval.
DFM Feedback: Specifics vs. Generic Approval
Generic approval reads like “drawings reviewed, no issues.” Specific feedback names features: a hole too close to a bend line, a thin web that will distort during cutting, a tight tolerance on a non-functional contour that adds inspection cost. Specific feedback proves the shop loaded your geometry and applied process knowledge to it. Treat a response with zero questions and zero comments as a warning sign rather than a convenience — complex drawings almost always contain at least one decision worth confirming.
Quote Lines You Can Audit
An auditable quote separates material, cutting (cut length or machine time), secondary operations (deburring, tapping, hardware, welding), finishing, inspection, and packing. It also states the assumptions it priced: material availability, sheet surface condition (oiled or dry, for example), tolerance class, and what triggers a requote. A single lump sum with no assumptions is a number you cannot compare against anything — and cannot hold anyone to later.
The Quality of Their Questions
The questions a supplier asks are free evidence. “Which dimensions are critical to assembly?” “Is this edge welded or sealed later?” “Is this the cosmetic face?” — these show the shop reads a drawing the way a production engineer does. Silence on fit and function usually means the job will be run exactly as drawn, including the parts of the drawing that were mistakes.
How to Verify Laser Cutting Capability Against Your Drawing
Machine lists describe capacity in general. Your part needs capability in particular. Three checks convert a brochure into a verdict.
Material, Thickness, and Bed Size
Confirm the provider regularly cuts your exact material family. Cold-rolled steel, 304 stainless, and 5052 aluminum behave differently under the beam, and parameter habits carry between jobs. Fiber laser systems typically reach about 20 mm on mild steel and roughly 12–15 mm on stainless with acceptable edge quality; beyond that, cut quality and speed fall off sharply. Bed size matters twice: once for your part envelope, and again for nesting yield, which quietly drives unit price on flat parts.
Kerf, Taper, and Tolerance Evidence
Kerf — the width of material the beam removes — runs about 0.1–0.3 mm depending on source, thickness, and assist gas. On thicker stock the cut face is rarely perfectly square: taper, a small angular difference between the top and bottom of the cut, appears. Neither is a defect, but both enter your tolerance chain. Laser cutting on sheet commonly holds ±0.1 mm on cut features, but do not accept that as a blanket promise. Ask instead for measured results on features like yours — hole diameters, cut-out spacing, profile position relative to datums. A supplier who claims ±0.1 mm on everything without reviewing your drawing has not understood it.
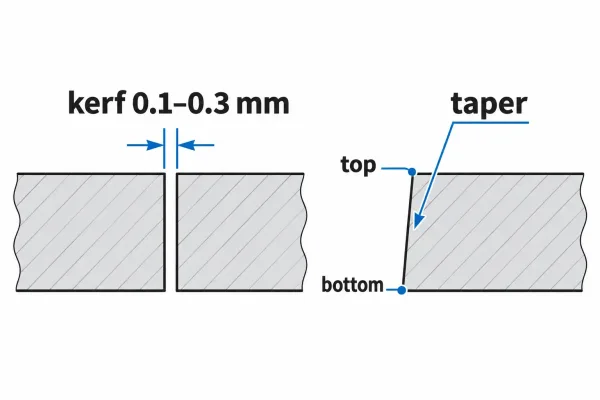
Kerf is the width of material the beam removes; taper is the small angular difference between the top and bottom of the cut.
Edge Condition and Heat Effects
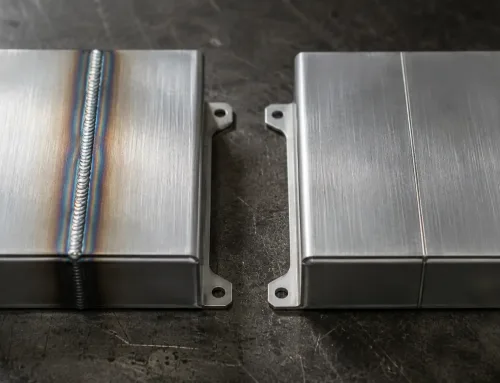
Cutting is a thermal process. Depending on parameters and gas, edges may carry dross (re-solidified melt), a narrow heat-affected zone (HAZ) where the microstructure changes, and oxide discoloration — especially on stainless. If the edge is welded, painted, or sealed later, these conditions decide whether the next operation succeeds. Ask to see magnified cut edges from a comparable job, and agree on the edge condition in writing: as-cut, deburred, or dressed. For appearance-critical parts, confirm the reference face and grain direction expectations at the same time.
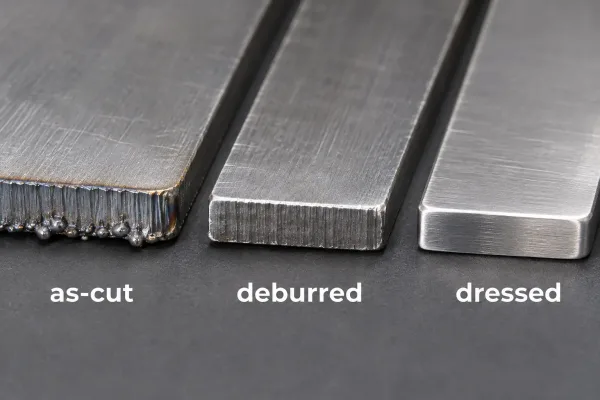
Three edge conditions side by side: as-cut with dross, deburred, and dressed — the condition to agree in writing before production.
What First Articles Need to Prove
A first article — the first part or small set produced to verify the process — is your strongest evidence stage. Approve it on data, not on the fact that it looks right.
Dimensional Evidence on the Sample
Ask for recorded measurements on your critical-to-quality (CTQ) dimensions: the features that drive fit, function, or assembly. Calipers, height gauges, and optical projectors cover most sheet metal features; you need the numbers, not the instrument brand. A report that says “all dimensions within tolerance” without values proves little. A report with nominal, measured, and deviation per feature shows where the process actually sits inside its band — near the middle, or living at the edge.
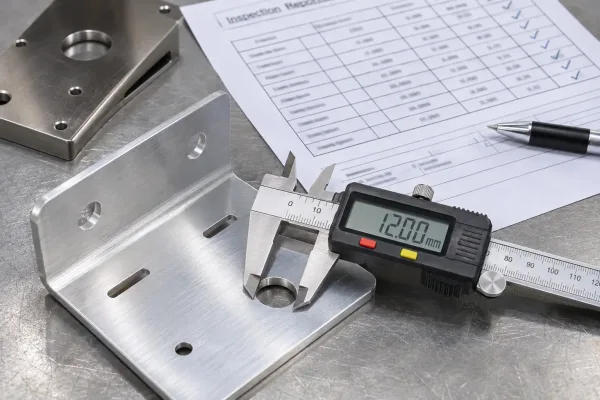
First-article check: recorded measurements on critical dimensions, not a visual pass.
Edge and Surface Checks
Run the edge checklist agreed in the capability stage: dross, striation (the cut-face texture pattern), heat-affected zone width where relevant, and discoloration on cosmetic faces. Check the sample against the drawing notes as well — protective film or no-scratch callouts must actually be followed. Edge and surface problems rarely improve between sample and production; they repeat.
What Sample Approval Does Not Prove
One good article proves the shop can make one good part. It does not prove lot-to-lot consistency, and it does not prove the batch will hold after a material change, a nozzle change, or a shift change. Before production release, ask what stays fixed in the machine program, how first-piece checks run in production, and whether inspection records ship with the lot. Sample approval and batch control are two different questions. Both need answers.
Quality Records Worth Requesting
Paperwork does not replace parts, but the right records show how a supplier controls variation — and what you can verify after delivery.
Inspection and First-Article Records
For production, request a dimensional inspection report against a sampling plan agreed in advance: 100% on CTQs where volume allows, otherwise a defined sample with the acceptance rule stated before the lot is built. “We always check” is a claim. A signed record with measured values is evidence.
Material Certificates and Traceability
Ask for material certificates to EN 10204 3.1 — the mill certificate confirming grade and mechanical properties for the actual batch — linked to the job by heat or lot number, rather than a generic certificate of conformance. Traceability matters when a corrosion or strength issue appears months later: without the batch link, the investigation stops at “it was stainless steel.” State this requirement at RFQ, not at delivery. Certificates retrieved after the fact are slow, and sometimes impossible.
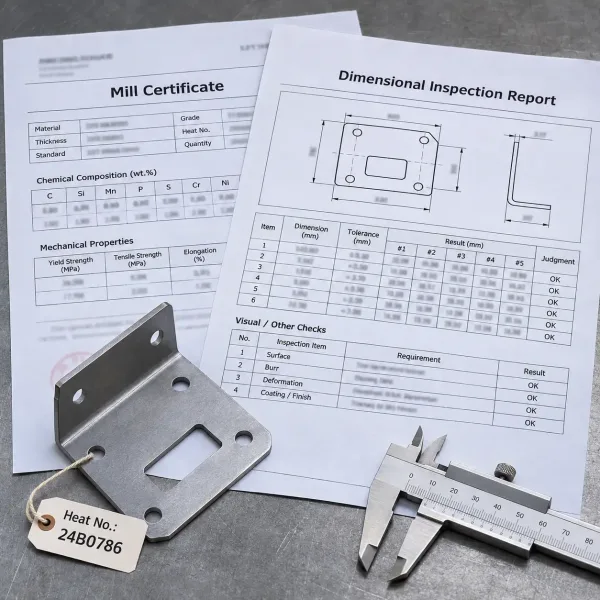
EN 10204 3.1 material certificate and inspection records linked to the job by heat or lot number.
Stage Gates: From Shortlist to Production Release
Weight the evidence by stage instead of scoring suppliers once on a spreadsheet. The table below maps each stage to the evidence worth collecting and the condition for passing it.
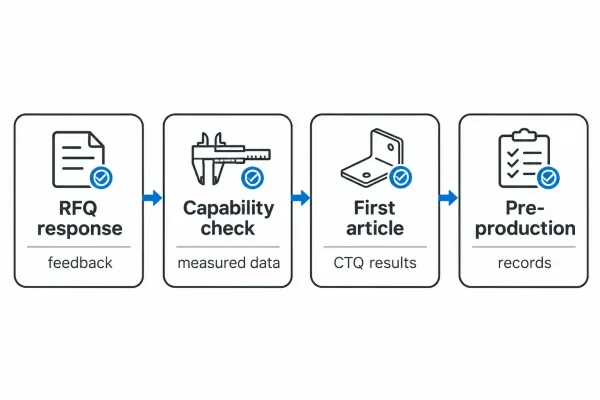
Evidence collects stage by stage: RFQ response, capability check, first article, and pre-production.
| Stage | Evidence to collect | Pass condition |
|---|---|---|
| RFQ response | Feature-level DFM feedback, auditable quote lines, informed questions | Issues named at feature level; assumptions written down |
| Capability check | Material and thickness track record, measured results on similar features, edge samples | Evidence covers your part’s requirements, not generic claims |
| First article | Recorded CTQ measurements, edge and surface conformance | CTQs inside tolerance with margin; agreed edge condition met |
| Pre-production | Inspection plan, material certificates, program freeze and change control | Records defined before the lot; traceability confirmed |
Gates work in one direction. A supplier that fails the RFQ stage rarely repairs it at sample stage, because the underlying discipline is missing — and strong RFQ feedback consistently predicts fewer surprises later.
Red Flags That End the Evaluation
Some findings justify stopping, whatever the price: flat quotes that cannot name their assumptions; refusal to provide measured results from comparable work; blanket tolerance promises without drawing review; no inspection records offered even for paid samples; dismissive answers to legitimate engineering questions. Each signals the same root problem — evidence is not part of how that shop works. An evaluation that continues past these findings is not being thorough. It is being slow.
The Pre-Order Evaluation Checklist
Use this list at the end of the shortlist stage, before any purchase order is released:
- Part requirements written down: material, thickness, tolerance class, edge condition, cosmetic face, secondary operations
- DFM feedback received at feature level, with open questions answered
- Quote split into material / cutting / secondary / finishing / inspection, with assumptions stated
- Tolerance evidence from comparable features — measured values, not brochure claims
- Edge samples reviewed at magnification against the agreed condition
- First-article plan defined: CTQ list, measuring method, acceptance rule
- Production inspection plan and sampling rule agreed
- Material certificates to EN 10204 3.1 requested and linked to the job
- Red-flag scan completed on quote, feedback, and communication quality
If your package is heading out for quotes and you want a manufacturing read on the points worth specifying — tolerance callouts, edge condition, inspection scope — SR-MFG reviews drawings at RFQ stage and returns concrete notes before the numbers arrive.