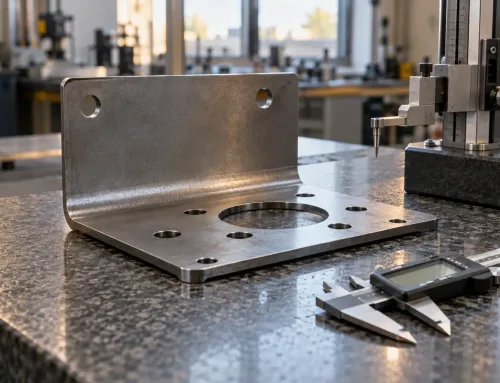
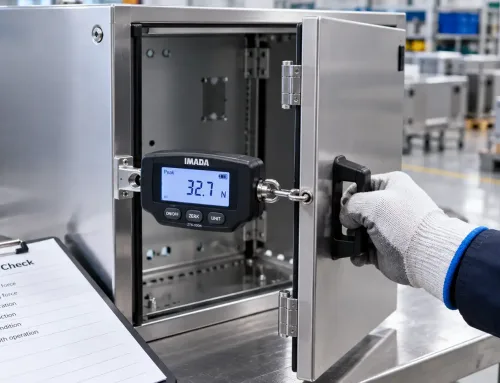
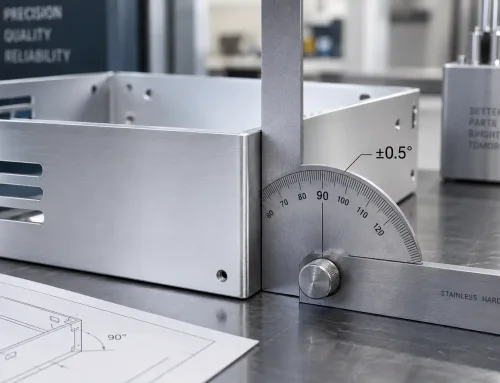
A batch of sheet metal brackets sits on the inspection bench. Three scratches, one dent, and one hole drilled 0.8 mm off position. The inspector marks them critical, major, and minor on the report. The lot now either ships or it does not — and the decision rests on those three marks.
That is the part most people miss. Defect classification is easy to file as a labeling exercise: sort the findings, fill the columns, close the report. But a class label only matters because of what it triggers. Classification is the rule that turns “here is what we found” into “here is what happens to the lot.”
Classification Is a Decision Rule, Not a Label
An inspection finding without a class has no consequence. A class without agreed consequences does not decide anything either. The two only work as a pair: the class names the severity, and the acceptance rule attached to it tells everyone whether the part ships, gets reworked, or gets rejected.
Treating critical, major, and minor as descriptive adjectives is what causes most receipt disputes. “Major” is not a synonym for “bad.” It is an input to a decision that should have been defined before the inspector picked up a gauge.
What Defect Classification Means in Manufacturing QC
Defect classification is the process of sorting a nonconformance — any finding that departs from the drawing or specification — into a predefined severity class according to the consequence it creates. Three separate actions are often blurred together on a shop floor:
- Detection answers: what did we find?
- Classification answers: how serious is it for this part?
- Disposition answers: what happens to the lot?
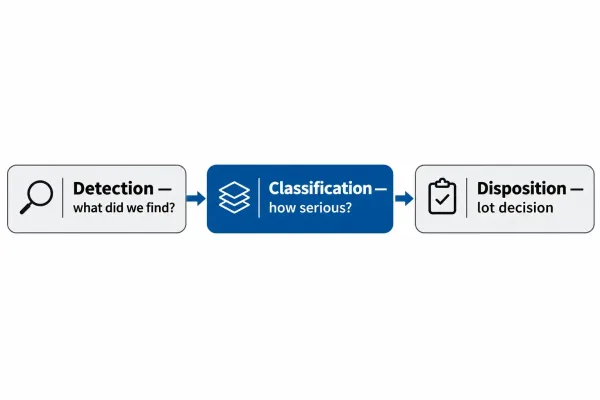
The three separate actions in defect handling: detection finds the nonconformance, classification assigns its severity class, and disposition decides the lot’s outcome.
Only the second action is classification. Keep the three apart and the acceptance logic downstream stays clean; merge them and every finding turns into an argument.
What Actually Decides the Class
The class is not decided by how a defect looks or how large it measures. It is decided by what the defect threatens.
The Consequence Test: Function, Safety, Fit, Appearance
Run every finding through a consequence test, from most severe to least:
- Critical — the defect creates a safety hazard, a regulatory noncompliance, or a functional failure. The part cannot do its intended job, or it puts the user at risk.
- Major — the defect degrades function, performance, or fit beyond the drawing requirement, without immediate hazard or outright failure.
- Minor — the defect affects appearance only, with no impact on function, safety, or assembly.
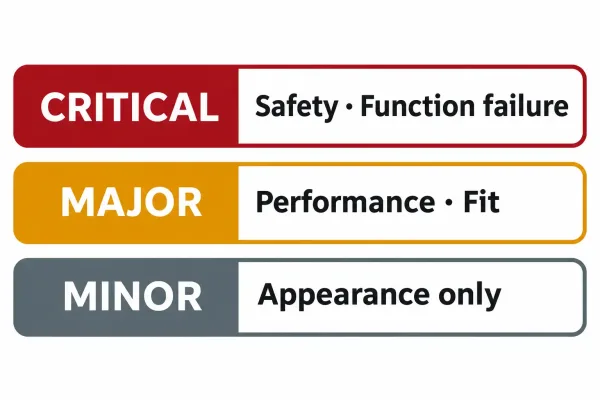
The consequence test ranks findings by what they threaten: safety or function failure (critical), performance or fit (major), appearance only (minor).
The order matters. If a finding could sit in two classes, the consequence decides — not the inspector’s impression of size.
Why the Same Defect Can Land in Different Classes
A 5 mm scratch is not a class. Its location and job are. On a hidden internal face of a cabinet, the same scratch is minor or not a defect at all. On a sealing surface it becomes major, because it can open a leak path. On a visible cosmetic panel judged against an agreed appearance standard, it is major as well.
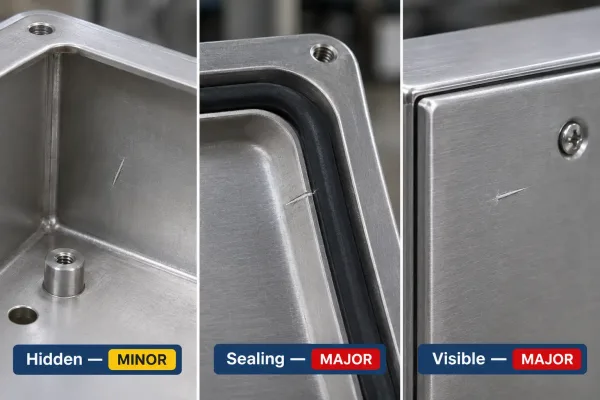
The same scratch classifies differently by location: minor on a hidden face, major on a sealing surface, and major on a visible panel.
Surface designation, the function that surface performs, and the product’s end use set the class. This is why generic defect lists copied from another product line rarely survive contact with a real inspection.
How the Class Drives the Acceptance Decision
Once a defect is sorted, the class maps to an acceptance outcome. The table below shows the common manufacturing convention; your purchase documents should state it explicitly rather than leave it to convention.
| Class | Typical acceptance consequence | Who can waive |
|---|---|---|
| Critical | Lot rejected or held; zero acceptance is the norm | Not routine QC — design or regulatory authority only |
| Major | Acceptable only within an agreed AQL, or after rework | Buyer quality, via written concession |
| Minor | Ships within the agreed AQL limit; usually non-blocking | Supplier QC within limit; buyer notified |
AQL (Acceptable Quality Limit) is the maximum defect rate a sampling plan tolerates for a given class. Critical defects typically carry an AQL of zero: one finding stops the lot. Major and minor defects follow the limits agreed in the contract or inspection plan — which is exactly why those limits must be written before production, not negotiated at the loading dock.
How This Looks on Real Sheet Metal Parts
Generic examples like “scratches and dents” are where most explanations stop. On fabricated sheet metal, findings from the same part sort very differently:
- Edge burr — minor on most deburred parts; major if the burr blocks assembly or cuts a wire or gasket; critical if it creates a laceration hazard on a user-accessible edge.
- Scratch through powder coating — minor on a hidden face; major on a visible panel when the finish specification is cosmetic; critical if the coating is the corrosion barrier on an outdoor enclosure and the substrate is exposed.
- Hole position 0.8 mm off — minor if the hole is clearance for an oversized fastener and assembly is unaffected; major if it shifts a mounted component out of tolerance; critical if it makes assembly impossible or loads a structural fastener incorrectly.
- Weld undercut on a structural seam — major at minimum; critical on a pressure or safety-critical joint.
- Bend angle 1.5° out of tolerance — major when it degrades fit; critical when the flange interferes with an installed component.
- Dent on a non-visible internal rib — minor, or not a defect, if no function is affected.
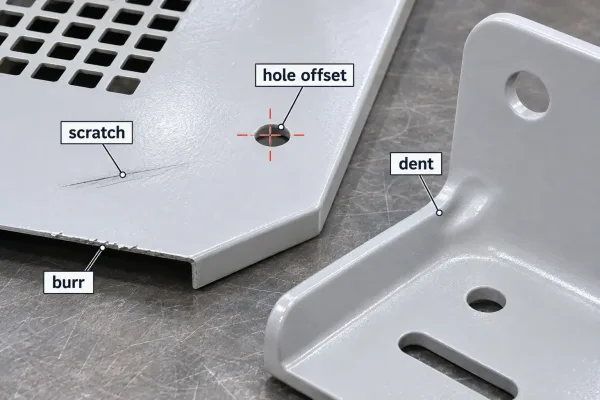
Typical sheet metal findings with labels: edge burr, scratch through coating, off-position mounting hole, and a dent on a flange.
The sorting rule is the same in every line: look at what the defect compromises, not at the defect alone.
Write the Rules Before the First Article Ships
What Belongs in the Drawing Note, RFQ, and PO
Classification only works if the classes travel with the order. Before quotation, the following should appear in the drawing package, RFQ, or purchase order:
- The three class definitions, written against your part’s surfaces and functions
- The acceptance consequence for each class (zero acceptance for critical; AQL or rework path for major; AQL limit for minor)
- Reference to appearance limit samples wherever cosmetic surfaces are judged visually
- Who holds final acceptance authority
A manufacturing review of the drawing at RFQ stage is where this pays off: the supplier quotes against the same rules the inspector will use, and the assumptions on both sides match.
Locking Boundary Samples at First Article
A boundary sample is an agreed physical example of the accept/reject edge for a subjective call — a scratch length, a discoloration, a dent depth. First article is the moment to set it. Once agreed, batch inspection compares against a fixed reference instead of shifting judgment, and the “is this major or minor” conversation largely disappears.
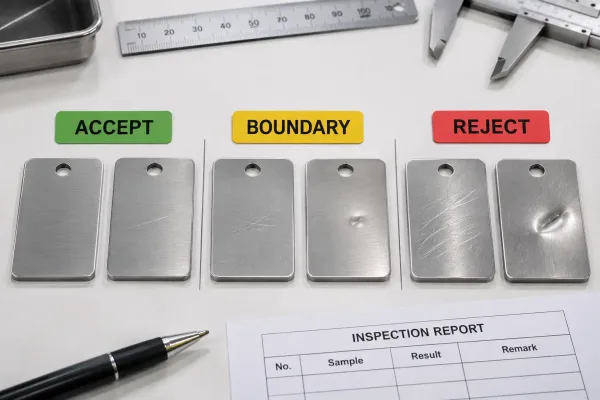
Boundary samples at first article: graded sample coupons grouped as accept, boundary, and reject references.
When Buyer and Supplier Classify the Same Defect Differently
Disagreements resolve along one path, in order:
- Check the written definitions first. Most conflicts end here: the drawing or PO already assigns a class to this surface and this consequence.
- Re-run the consequence test together. Ask what the defect threatens on this part — function, safety, fit, or appearance — and classify from the answer, not from precedent on another job.
- Fall back to a written concession path. If the class is genuinely ambiguous, the buyer either accepts the deviation formally or rejects it. Final acceptance authority for product conformity normally sits with the buyer, but the argument should cite the agreed documents, not opinion.
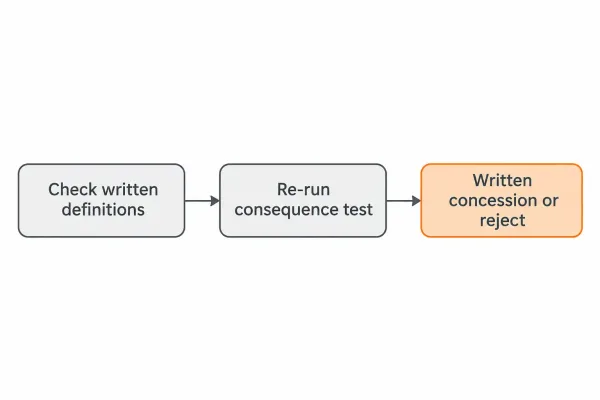
Dispute resolution in order: check the written definitions, re-run the consequence test, then use the written concession path.
If these steps are not defined before production, the negotiation happens at goods-in with a truck waiting — the most expensive time to have it.
FAQs
Before your next order goes out, fix the three classes and their acceptance consequences in writing, and set boundary samples at first article. If you want the inspection terms checked before RFQ, SR-MFG’s engineering team reviews drawings and acceptance requirements during quotation — one set of assumptions on both sides, fewer surprises at receipt.