Every coated part that leaves a fabrication shop has a color. Not every buyer and supplier agree on what counts as the same color. Phrases like “slightly lighter” or “close enough” hold up in a design review and collapse on a receiving dock, where two inspectors can look at the same part against the same master sample and reach opposite conclusions.
Delta E (written ΔE) is what settles that argument with a number. This glossary entry explains what the value actually represents, where it comes from, and how it functions in acceptance decisions on finished parts.
Why “Close Enough” Is Not a Color Specification
Color judgment is subjective in ways people underestimate. Illumination changes the impression — a powder-coated panel that matches under daylight can look off under warm shop lighting. Memory is worse: the eye compares what is in front of it to a recollection of the approved sample, not the sample itself.
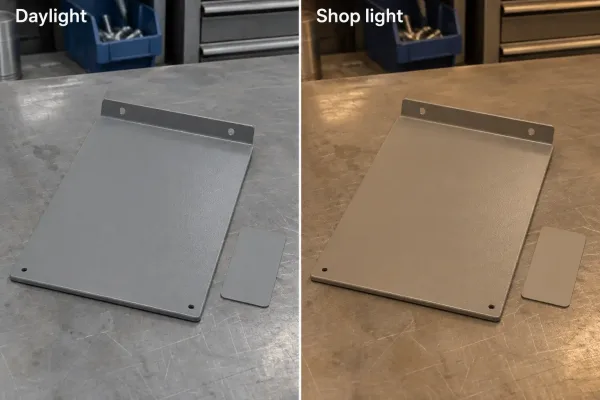
The same panel and reference chip under daylight (left) and warm shop light (right).
When a purchase order only says “color to match approved sample,” neither side has an objective referee. The supplier judges one way, the buyer another, and a rejected batch becomes a negotiation rather than a measurement.
A shared number removes that ambiguity. The job of ΔE is narrow and practical: it converts “do these two colors match?” into a value both parties can check with the same instrument and the same rules.
What Delta E Actually Measures
ΔE is the calculated distance between two colors in the CIELAB color space (L*a*b*) — the color model most manufacturing color instruments report. One number summarizes the total difference: the lower the ΔE, the closer the two colors.
The definition has an implication that is easy to miss. ΔE is a difference between two readings — a production part and a reference. It is not a property of a single part. A part does not “have” a ΔE of 1.2; it has a ΔE of 1.2 relative to a master sample, a color chip, or a specified standard.
In the common CIE76 formula (ΔE*ab), the total is the straight-line distance between two points in L*a*b* space, assembled from three component differences.
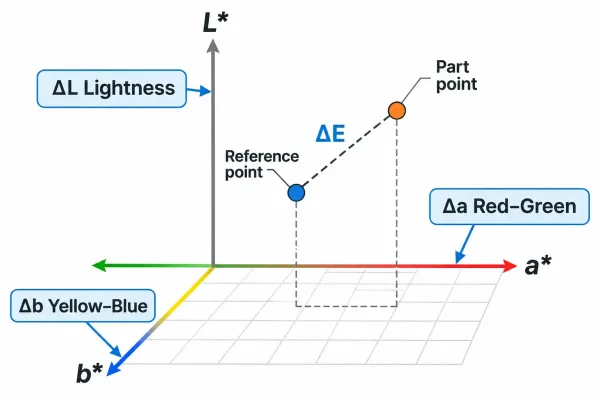
The three Lab* axes and the ΔE distance between a reference point and a part point.
The Three Components
The CIELAB model describes any color on three axes. Each Δ component is the signed difference between the part reading and the reference:
| Component | Axis | Positive means | Negative means |
|---|---|---|---|
| ΔL* | Lightness | Lighter than reference | Darker than reference |
| Δa* | Red–green | Redder / less green | Greener / less red |
| Δb* | Yellow–blue | Yellower / less blue | Bluer / less yellow |
The total ΔE combines all three into a single distance. That compression is convenient and also lossy: a part can be slightly lighter, slightly greener, and slightly more yellow and still show a modest total — which is why the components matter once you read an actual report.
What the Numbers Mean in Practice
Delta E values track surprisingly well with what the eye notices. The ranges below are widely used as a working translation:
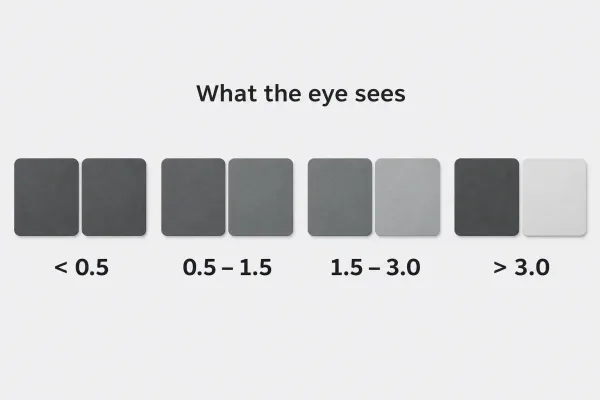
Four swatch pairs, each step showing a larger ΔE gap from left to right.
| ΔE range | What an observer typically sees |
|---|---|
| < 0.5 | Not perceptible, even with parts side by side |
| 0.5 – 1.5 | Perceptible only on close, deliberate comparison |
| 1.5 – 3.0 | Noticeable at a glance when parts are placed together |
| > 3.0 | Obvious difference — reads as a different color |
Two cautions apply to this table.
First, visibility is not acceptability. A shift of ΔE 2.0 may be unacceptable on a cosmetic enclosure face and entirely fine on an internal bracket. The table describes what people see; it does not decide what a project can live with.
Second, perception is color-dependent. Shifts in neutral grays and in saturated blues are often noticed at lower ΔE values than shifts in mid-tone colors. An instrument treats all three the same; your customer may not.
Use the table to understand the number. Set the pass/fail limit per surface and per function.
Where the Number Comes From — and Why the Method Must Be Agreed
A ΔE value begins with instrument readings. A spectrophotometer or colorimeter measures the surface and reports coordinates in L*a*b*; the calculated difference between two readings produces ΔE. There is no manual equivalent — “looking close” does not generate a number. ASTM D2244 covers the standard practice for calculating color differences and color tolerances from instrumentally measured coordinates.
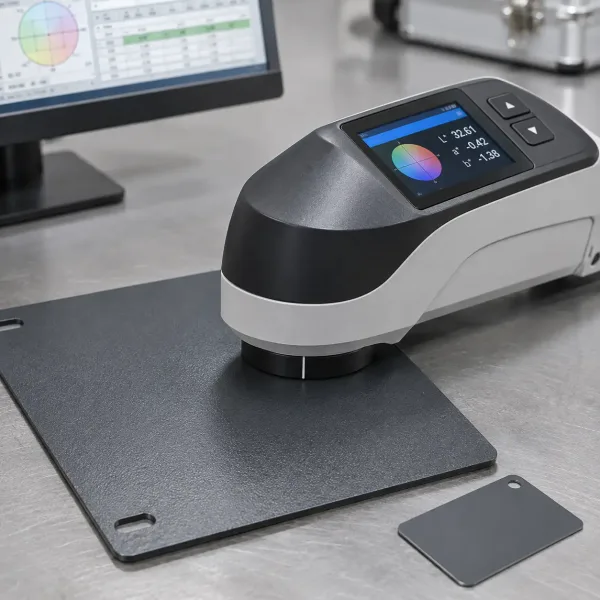
A spectrophotometer reading the coated panel surface, with a reference chip on the bench.
Here is the part that matters for procurement: the same part can produce different ΔE values under different measurement conditions. The number is only comparable when the method is fixed. This is why a complete specification names conditions, not just a limit.
What Changes the Reading
- Illuminant — the defined light source for the measurement, commonly D65 (daylight, ~6500 K). A part measured under D65 and judged under warm shop light can pass and fail the same eyes in the same afternoon.
- Geometry — how the instrument illuminates and views the surface; 45°/0° and d/8° are common. Glossy and textured coatings respond differently across geometries.
- Specular component — whether gloss is included in the reading (SCI) or excluded (SCE). On high-gloss powder coat, this choice alone can move ΔE.
- Measurement location — a flat face, a formed edge, and an area near a weld bead are three different surfaces. Readings must be taken at agreed points.
If a drawing calls for ΔE ≤ 1.5 but fixes none of these, two suppliers can disagree about whether a part passed — and neither is wrong about the math. The conditions are part of the requirement.
Reading the Three Components on a Report
Inspection reports usually list ΔL*, Δa*, Δb* beside the total ΔE. The components tell you which direction the color moved, and that is what turns a verdict into a diagnosis.
Consider two production panels measured against the same master sample:
| Panel A | Panel B | |
|---|---|---|
| ΔL* | −1.8 | +0.2 |
| Δa* | +0.4 | +1.6 |
| Δb* | +0.3 | −0.5 |
| ΔE | 1.9 | 1.7 |
By total alone, the two panels look similar — both under 2.0. The components say otherwise. Panel A is almost entirely a lightness problem: the panel reads darker than the master, barely off in hue. If anything is adjusted, it is tone. Panel B is a hue problem: nearly all of its error sits on the red–green axis, so the panel reads off in tint even though its total is lower.
Ranked by ΔE alone, Panel B would look marginally better. For diagnosis and correction, Panel A is the easier case and Panel B is the real color-matching problem. The total decides pass/fail; the components tell you what to fix.
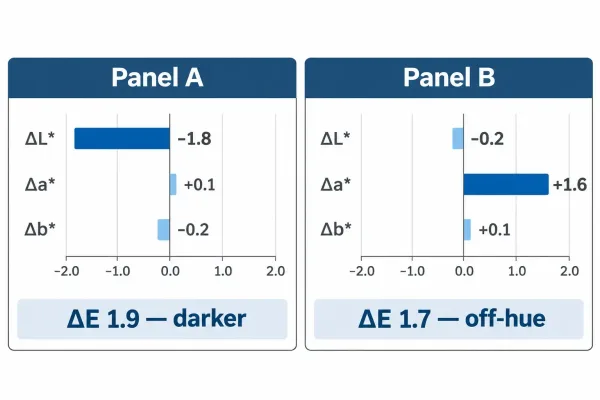
Panel A’s difference sits in ΔL*; Panel B’s sits in Δa*, despite similar totals.
What ΔE Does in an Acceptance Decision
At incoming inspection, a ΔE limit is a decision rule: measure the production part against the agreed reference, under agreed conditions, and compare the result to the agreed threshold. Passing means the part is within tolerance of that reference. It does not mean the color is correct in any absolute sense — if the reference itself is wrong, a passing ΔE proves nothing.
Three boundaries are worth stating plainly:
- It is point-specific. A pass at one measurement location says nothing about unmeasured areas. Cosmetic faces and visible seams need their own points if they matter.
- It is piece-specific. A first-article pass proves that part was acceptable. It does not guarantee part 500. Batch drift comes from coating batch variation, film thickness, and cure — none of which a one-time ΔE reading measures.
- It is color-specific. ΔE judges color coordinates only. Texture, gloss level, and surface waviness can look wrong on a part that passes on color. Appearance complaints often survive a passing report.
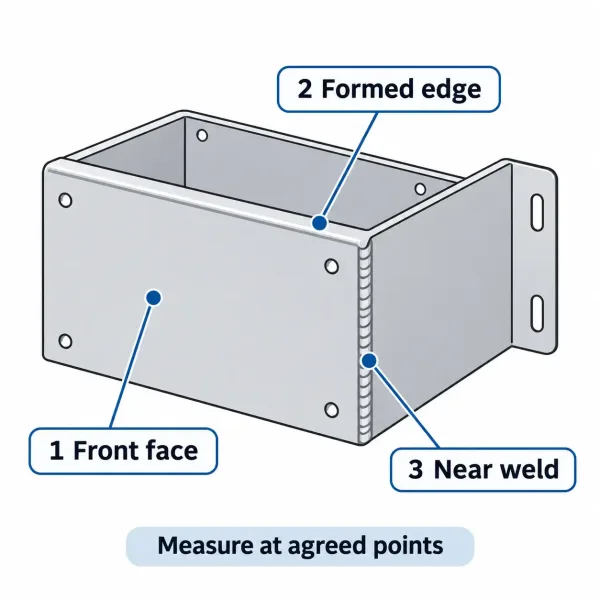
Three agreed measurement locations on a coated enclosure: front face, formed edge, and near the weld.
What prevents disputes is not a tighter number but a complete one. Before the first order, fix four things in the drawing or PO: the reference (master sample or color standard), the formula version, the measurement conditions, and the limit. Choosing the limit value is its own decision; understanding what the number does is the part that keeps that decision honest.
FAQs
Key Takeaways
- ΔE is the distance between two colors in L*a*b* space — lower is closer, and the value is always relative to a reference.
- Working ranges (< 0.5 imperceptible; 1.5–3.0 noticeable at a glance) translate the number into human terms; the acceptance limit remains a project decision.
- The reading is only comparable when illuminant, geometry, gloss handling, and measurement points are fixed.
- ΔL*, Δa*, Δb* show which direction the color moved — the diagnosis a total alone cannot give.
- In acceptance, ΔE proves closeness to an agreed reference at an agreed point. It does not prove absolute correctness, batch consistency, or texture match.
Specify the reference, the formula, the conditions, and the limit as one set. That combination is what turns ΔE from a line in a report into a decision both sides can stand behind.