A warehouse can meet a written relative humidity target and still send flash-rusted sheet to the laser. The gap is rarely “we forgot to buy a dehumidifier.” It is condensation on cold stock, a broken pack after a weekend, or dry CRS that was never supposed to sit un-oiled in coastal air.
Humidity control for sheet metal stock is not a facilities slogan. It is a set of storage and receiving rules that keep raw material fit for cutting, welding, and coating.
Why Sheet Metal Stock Is Not Just Warehouse Inventory
Sheet metal stock is production inventory. Its surface condition is a manufacturing input, not a cosmetic detail.
Once oxide, flash rust, or oil contamination is on the face, it shows up later as cut-edge issues, weld porosity risk, coating adhesion failures, or extra prep labor. Those costs land on the job traveler, not on the warehouse P&L.
Humidity damage is also cumulative. A part that “looks fine” on the rack can still need grinding or rework after a humid week. For low-volume OEM work, a spoiled sheet often means a delayed nest and a missed ship date.
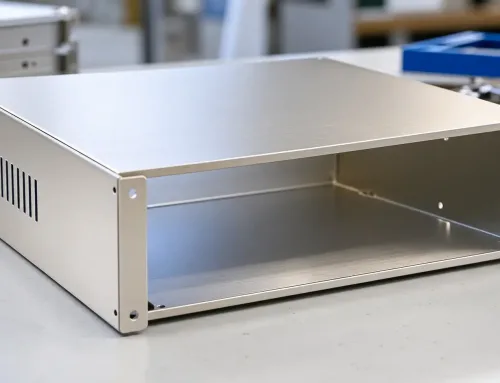
From rack to laser bed: humidity damage becomes scrap or rework the moment surface condition blocks a process step—degrease, weld prep, powder coat, or cosmetic face on an enclosure.
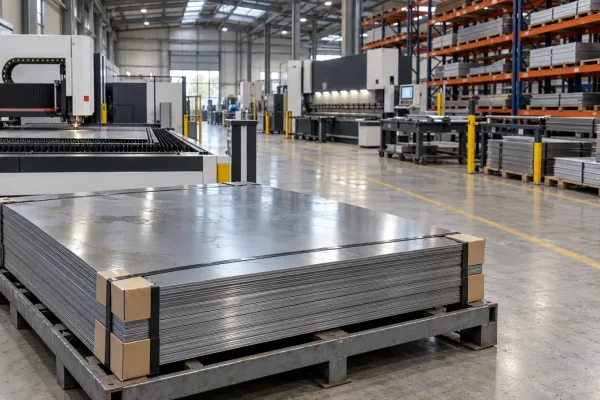
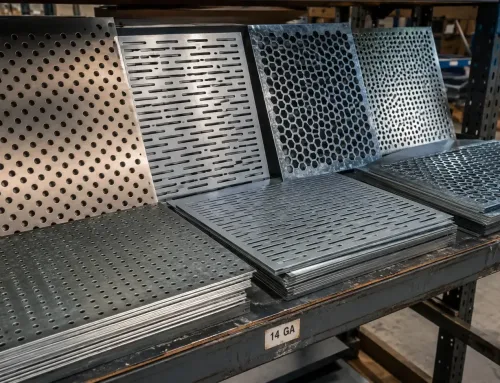
Raw sheet packs staged near production so humidity damage is controlled before cutting.
Why a Target RH Alone Does Not Keep Sheet Metal Dry
Relative humidity (RH) measures how saturated the air is at a given temperature. It does not tell you whether water will condense on metal.
Dew point vs relative humidity on the shop floor
Dew point is the temperature at which air can no longer hold its moisture and water forms on surfaces. If sheet temperature falls below the dew point of the room air, condensation forms even when the room RH looks acceptable.
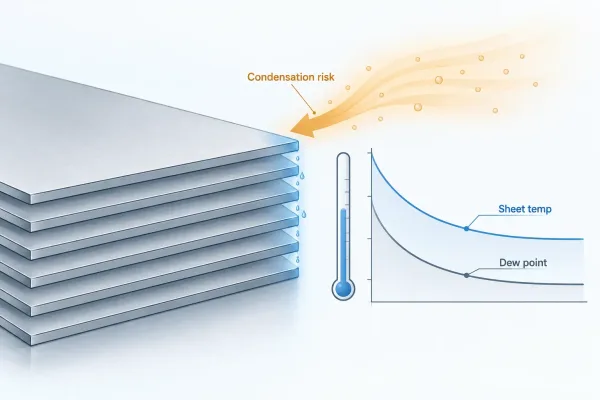
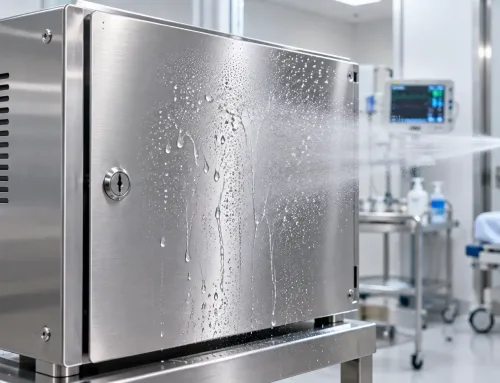
Condensation forms when sheet temperature falls below the air dew point, even if RH looks acceptable.
Typical storage guidance aims for a dry, stable bay—often below about 60% RH where practical, with temperature held steady enough that packs and pallets do not swing through the dew point. Those numbers are starting points, not universal law. Climate, season, and material state can force a tighter or looser target.
When condensation actually forms
High-risk windows are easy to miss:
- Cold sheet or packs moved into warm, humid air (morning unloads, winter-to-summer handoffs)
- Overnight temperature drops that cool metal faster than the room
- Opening a sealed pack so warm ambient air hits cold faces
- Gaps in VCI or stretch wrap that let humid air reach bare metal
A stable 18–24°C bay is easier to manage than a shop that swings 10°C in a day, because fewer surfaces cross the dew point. Sensor placement matters too: log near the stock, not only at a ceiling return.
How Material Type Changes Humidity Risk
Not every alloy fails the same way at the same RH. Storage rules should follow the metal and its surface state.
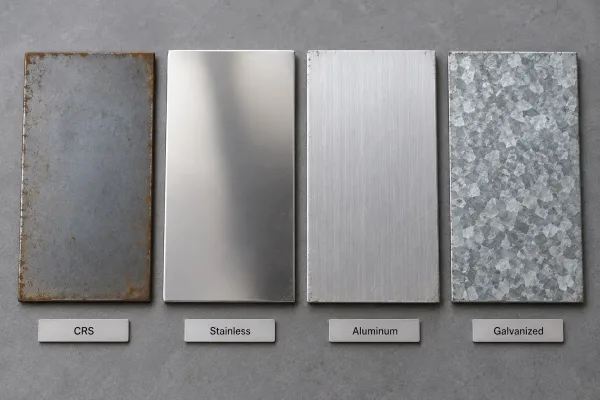
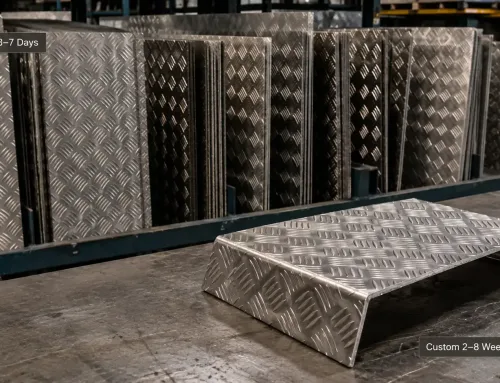
CRS, stainless, aluminum, and galvanized sheets face different humidity risks in storage.
| Material | Typical humidity risk | Storage emphasis |
|---|---|---|
| Cold-rolled steel (CRS), dry | High flash-rust risk on bare faces | Short dry exposure; oil, VCI, or fast turnover |
| HRPO / oiled steel | Oil film helps, but packs still trap moisture | Keep wrap intact; do not leave oil-free blanks stacked wet |
| Stainless steel | Lower general rust risk; staining and contamination still matter | Clean, dry racks; keep free of carbon-steel dust |
| Aluminum | Whitish oxide and water-stain on cosmetic faces | Dry, covered; avoid condensation on bright finishes |
| Galvanized / coated | Coating helps; cut edges and damaged areas remain vulnerable | Protect edges and damaged spots; control pack integrity |
Thin sheet deserves extra care. It has less mass to buffer temperature swings and shows handling marks more easily. A humidity policy for heavy plate will not protect 0.8 mm cosmetic panels.
Surface Condition and Packaging: The Other Half of Humidity Control
Humidity policy and surface condition have to be specified together. A dry CRS order stored like oiled stock will not behave the same.
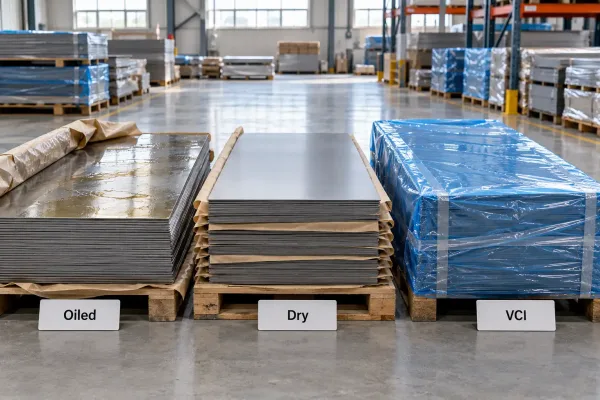
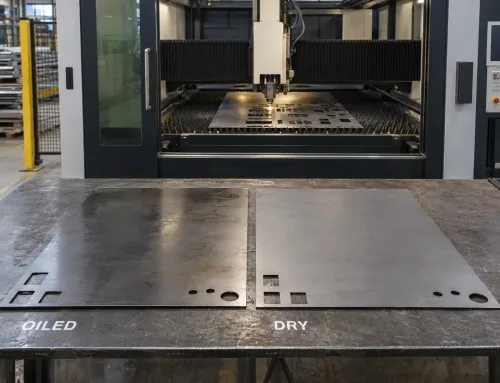
Oiled, dry, and VCI packs each assume a different warehouse exposure limit.
Oiled, dry, and VCI: what each one assumes
- Oiled stock assumes oil remains on faces through handling. Solvent wipe before some welds or coatings is expected later, but the oil is part of the storage plan.
- Dry stock assumes low exposure time, controlled air, and quick use. It is a poor fit for long holds in humid seasons unless packs stay sealed and climate is controlled.
- VCI (vapor corrosion inhibitor) paper or film assumes continuous contact and intact wrapping. Once the pack is opened and left open, VCI no longer replaces humidity control.
Broken stretch wrap, torn VCI, or open bundles after a partial pick are common root causes in “we controlled humidity” claims. Packaging is part of the corrosion barrier, not just transport protection.
Storage Decision Factors: Temperature, Layout, and Turnover
Facilities cannot always build a fully conditioned warehouse. Decision factors still apply in mixed shops.
A practical target range—and why one number does not fit every shop
Use RH and temperature as a pair. Keep the bay dry enough to limit corrosion chemistry and stable enough that stock does not cross dew point. For many fabrication environments that means a best-effort band near or below ~60% RH, with heating or dehumidification sized for the actual volume and door cycles—not for a brochure case.
Coastal sites, monsoon seasons, and buildings with open dock doors need more margin than inland, climate-controlled plants. If the only tool is a small portable unit at one end of a long rack aisle, treat the log data as the real system state.
Monitoring that supports a decision
Minimum useful practice:
- Data loggers at stock height in the worst corner of the bay (not only by the HVAC unit)
- Alarms or weekly review when RH or temperature stays outside range
- Pack and face checks at receiving and before first cut
- FIFO or “use the most exposed stock first” when humidity control is imperfect
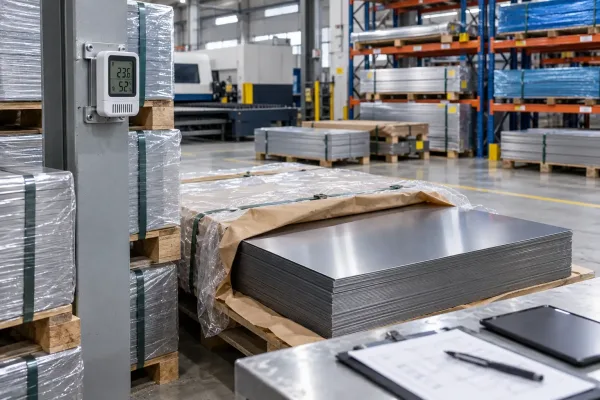
RH logging at stock height and pack checks support acceptance and scrap decisions.
Without records, “it rusted at your plant” is an opinion. With time-stamped logs and pack photos, it is an engineering discussion.
What Buyers Should Put on the RFQ and Check at Receiving
Procurement can prevent most storage disputes at the drawing and PO stage.
Specify:
- Material grade and thickness
- Surface condition (oiled, dry, HRPO, VCI, etc.)
- Cosmetic or no-scratch faces if humidity and handling both matter
- Whether long-term storage is expected before machining
- Receiving inspection for flash rust, pack damage, and oil condition
At receiving, photograph packs before full unwrap. If flash rust appears early, that evidence separates factory, carrier, and storage causes faster than a week of email.
For overseas sheet metal orders, agree in writing who controls humidity after delivery and which surface defects are acceptance criteria. That clause is cheaper than a re-make.
Humidity Control Rules You Can Audit on the Floor
Use these as floor rules, not a slogan:
- Define RH and temperature targets for stock bays, and log them at material height.
- Match surface condition (oiled / dry / VCI) to hold time and climate—not to habit.
- Keep packs sealed until the material is staged for work; re-wrap partials the same shift.
- Store off the floor, under cover, away from open docks and cold exterior walls where possible.
- Stage cold material before opening if the room air is warmer and humid (condensation window).
- Run FIFO or prioritize the most exposed stock when conditions are imperfect.
- Inspect at receiving and before first cut; record pack condition and face condition with photos.
- Put surface condition, storage expectations, and acceptance notes on the RFQ or PO.
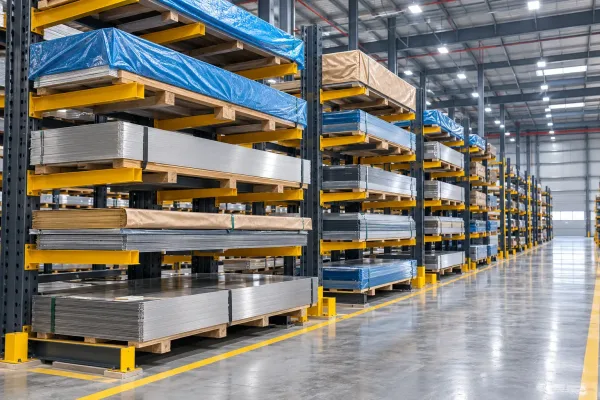
Sheet stock kept off the floor, covered, and organized for FIFO turnover.
If one rule fails, fix the pack or the bay before cutting. Humidity control only works when packaging, material state, and shop discipline point the same way.
FAQs